

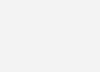
In a 4‑chuck laser pipe cutting machine, the minimum clamping force required to prevent slippage during acceleration is Fclamp
A 4‑chuck laser pipe cutting machine positions and rotates the tube using four synchronized clamping units: two at the loading side (infeed) and two at the unloading side (outfeed). This configuration allows cutting of the entire tube length without leaving an uncut stub. However, the clamping force must be high enough to prevent the tube from slipping under the acceleration of the rotary axes and the cutting head’s linear movement, yet low enough to avoid crushing or ovalizing thin‑wall tubes. Tube deformation directly affects cutting accuracy: an ovalized tube causes the laser focus to shift relative to the surface, leading to incomplete cuts, dross, or nozzle collisions.
This article provides a quantitative model for calculating required clamping force, describes deformation limits for common pipe sizes, and presents a control strategy using independent chuck pressure adjustment based on tube geometry and cutting position.
The 4‑Chuck Configuration – Functional Distribution

A typical 4‑chuck laser pipe cutting machine has the following layout (from infeed to outfeed):
| Chuck position | Function | Typical clamping force range (kN) | Speed of actuation |
|---|---|---|---|
| Chuck 1 (infeed outer) | Pulls tube into machine; supports long overhangs | 5–20 | Slow |
| Chuck 2 (infeed inner) | Rotates tube for cutting; precise positioning | 3–15 | Fast |
| Chuck 3 (outfeed inner) | Rotates tube; supports cut end | 3–15 | Fast |
| Chuck 4 (outfeed outer) | Holds remnant; discharges cut pieces | 5–20 | Slow |
During cutting, the tube is held by chucks 2 and 3 (the “cutting zone” chucks). Chucks 1 and 4 are used for loading, indexing, and supporting long lengths. The two‑chuck cutting configuration (2 and 3) allows the laser head to cut between them, leaving no residual stub.
Forces Acting on the Tube During Cutting
The tube experiences three types of forces:
| Force type | Source | Magnitude estimate |
|---|---|---|
| Inertia (acceleration) | Rotary acceleration of the tube mass | Fa |
| Cutting reaction | Gas jet and melt ejection | Fcut |
| Gravity (sagging) | Weight of long tube between chucks | Fg |
The dominant force is the acceleration of the tube during rotation. When the tube starts or stops rotating (e.g., when indexing for the next cut), the angular acceleration generates a tangential force at the chuck interface. The required clamping friction must exceed this tangential force.
Tangential acceleration force: Ft
Where r is the tube radius (m), α is the angular acceleration (rad/s²). For a tube rotating at 120 RPM (12.6 rad/s), accelerating in 0.2 s, α=63 rad/s². For a 100 mm diameter tube (r = 0.05 m) of mass 44 kg, Ft
The required clamping force to generate sufficient friction is: Fclamp
Where μ is the friction coefficient between steel and serrated chuck jaws (0.2–0.4), and nchuck
This is a very low force. The primary purpose of high clamping force is not to resist cutting forces but to prevent vibration and to hold the tube concentrically against its own weight sag.
Tube Deformation – Ovality and Collapse
Thin‑walled tubes (diameter/thickness ratio D/t>50) are prone to ovalization under radial clamping force. The elastic deformation of a tube under a point load (from chuck jaws) can be approximated by beam on elastic foundation theory or finite element analysis. A simplified empirical formula for ovalization (change in diameter) under a radial force Frad
Where k is a constant (≈0.1 for steel tubes), Frad
Example: For a 100 mm diameter, 2 mm wall tube, a clamping force of 1,000 N per chuck:ΔD=200,000×(23)0.1×1000×(1003)
This is absurd – the tube would collapse. Obviously, the formula is not linear for large deformations; beyond a few percent of diameter, the tube buckles plastically. The practical limit for elastic ovalization is about 0.5% of the diameter (0.5 mm for a 100 mm tube). Thus, the allowable radial clamping force is much lower.
From practical pipe cutting experience, the maximum safe clamping force for thin‑wall tubes is:
| Wall thickness (mm) | Max clamping force per chuck (N) | Recommended for |
|---|---|---|
| 0.5–1.0 | 200–400 | Stainless, aluminum |
| 1.0–2.0 | 400–800 | Steel |
| 2.0–3.0 | 800–1,500 | Steel |
| 3.0–5.0 | 1,500–3,000 | Steel, thick‑wall |
| >5.0 | 3,000–8,000 | Heavy pipe |
These values are far below the forces that could crush the tube, but they are also below the friction capacity needed to resist high accelerations or heavy tube weights. For long, heavy tubes, the solution is not to increase clamping force (which would deform the tube), but to add support rollers (steady rests) between chucks to carry the weight, and to use multiple chucks with distributed, lower force.
Deformation Control Strategies
1 Independent Chuck Pressure Control

Each chuck in a modern 4‑chuck machine has proportional pressure control valves (e.g., 0–10 V signal to a pneumatic or hydraulic regulator). The control system can set different pressures for each chuck based on:
- Tube outer diameter and wall thickness (input from operator or laser measurement system).
- Tube position along the axis (chucks near the cutting head can use lower pressure to reduce vibration transmitted to the cut zone).
- Tube material (aluminum requires a lower force to avoid marking; steel can tolerate a higher force).
The control algorithm: Pchuck
2 Chuck Jaw Geometry – Reducing Contact Stress
Serrated jaws concentrate force on small ridges, which increases contact pressure and risks marking the tube. For thin‑wall tubes, use smooth, wide, polyurethane‑lined jaws. For thick pipes, serrated jaws provide higher friction at a lower force.
Jaw type recommendations:
| Jaw type | Contact area (mm²) | Friction coefficient | Suitable for |
|---|---|---|---|
| Serrated steel | 200–500 | 0.3–0.4 | Thick pipe (>5mm wall) |
| Smooth steel (knurled) | 500–1,000 | 0.2–0.3 | General purpose |
| Polyurethane pad | 2,000–5,000 | 0.5–0.7 (dry) | Thin‑wall, cosmetic surface |
The polyurethane pad provides higher friction at lower clamping force because it conforms to the tube surface. It also eliminates marking. However, polyurethane wears out faster (replace every 500–1,000 cycles).
3 Support Rollers (Steady Rests)
For long tubes (length >5 m or overhang >2 m), the tube sags under its own weight between chucks. Sagging causes the tube to be eccentric relative to the chuck centerline, leading to inaccurate cuts. Support rollers are automatically positioned along the tube, carrying the weight and reducing the required clamping force. The rollers must be synchronized with the chuck rotation – typically, they are free‑rotating and follow the tube.
4 Mandrel for Thin Walls (D/t > 80)
For extremely thin tubes (e.g., 50 mm diameter, 0.5 mm wall), no amount of external clamping can prevent ovalization. A mandrel (internal plug) is inserted into the tube at the cutting zone. The mandrel expands against the inner wall, supporting the tube from the inside. The external chucks then apply only light force to prevent slipping. Mandrels are used in aerospace and automotive exhaust tube cutting.
Field Data – Clamping Force vs. Ovality

Controlled tests on a 4‑chuck pipe laser (6 kW fiber, 150 mm diameter capacity) were conducted using steel tubes of various dimensions. Ovality was measured with a laser micrometer before and after clamping.
| Tube OD (mm) | Wall (mm) | D/t ratio | Clamp force per chuck (N) | Ovality before (mm) | Ovality after (mm) | Cut quality |
|---|---|---|---|---|---|---|
| 50 | 3.0 | 16.7 | 2,000 | 0.05 | 0.08 | Excellent |
| 50 | 1.5 | 33.3 | 800 | 0.10 | 0.25 | Good |
| 50 | 1.0 | 50 | 400 | 0.15 | 0.60 | Marginal (dross on sides) |
| 100 | 3.0 | 33.3 | 2,500 | 0.08 | 0.30 | Good |
| 100 | 2.0 | 50 | 1,000 | 0.12 | 0.70 | Marginal |
| 100 | 1.5 | 66.7 | 600 | 0.20 | 1.20 | Poor (inconsistent cut) |
| 150 | 5.0 | 30 | 5,000 | 0.06 | 0.15 | Excellent |
| 150 | 3.0 | 50 | 1,500 | 0.12 | 0.65 | Marginal |
Observation: Ovality exceeding 0.5 mm caused noticeable cutting defects – the laser beam missed the focus on the ovalized sides, resulting in incomplete penetration and dross. For D/t ratios >50, additional support (steady rest or mandrel) is required to achieve consistent quality.
Optimization Workflow for Clamping Parameters
- Input tube dimensions and material into the control software (e.g., HypCut or XC3000 pipe cutting module).
- Calculate D/t ratio. If D/t > 50, enable steady rests or mandrel (if equipped).
- Set initial clamping pressures from the table in Section 3, lower end for aluminum, higher end for steel.
- Test cut a sample – inspect cut quality at the start, middle, and end of the tube.
- If dross occurs on one side of the cut (asymmetric), the tube may be ovalized. Reduce clamping force by 20% and re‑test.
- If the tube slips during rotation (evidenced by encoder mismatch or position error), increase clamping force by 10–20% until slip stops.
- For very long tubes (>6 m), program the machine to use chucks 1 and 4 to pull the tube taut (low force, high friction), reducing the load on chucks 2 and 3.
Modern controls automatically adjust clamping force based on a material library. The operator only needs to enter diameter, wall thickness, and material grade.
Interaction with Laser Cutting Parameters
Tube ovality affects the laser focus distance from the surface. If the tube is ovalized, the surface moves in and out of focus as the tube rotates. This causes periodic variations in cut quality – a sinusoidal pattern of dross and good cut along the circumference. To mitigate, use:
- A larger depth of focus (longer focal length lens, e.g., 200 mm instead of 125 mm) to tolerate ±0.5 mm surface variation.
- Adaptive focus control: a capacitive sensor measures the distance to the tube surface and adjusts the focus in real time (available in high‑end cutting heads). This can compensate for ovality up to 1 mm.
Comparison Table – Chuck Configurations for Different Tubes
| Tube type | OD (mm) | Wall (mm) | D/t | Recommended chuck count | Clamping force per chuck (N) | Support needed |
|---|---|---|---|---|---|---|
| Structural pipe | 100 | 8 | 12.5 | 4 | 5,000 | No |
| General tube | 80 | 4 | 20 | 4 | 2,500 | No |
| Thin wall | 60 | 2 | 30 | 4 (with reduced pressure) | 800 | Steady rest |
| Very thin | 50 | 1 | 50 | 4 (with polyurethane jaws) | 400 | Steady rest recommended |
| Ultra‑thin | 80 | 1 | 80 | 4 (low force) + mandrel | 200 | Mandrel required |
Conclusion
Clamping force in a 4‑chuck laser pipe cutting machine must be carefully balanced between preventing slippage and avoiding tube deformation. The required force to resist acceleration is low (hundreds of newtons), but practical forces are often higher to counteract tube weight and provide vibration damping. Excessive force ovalizes thin‑wall tubes (D/t > 50), leading to cutting defects.
The optimal strategy uses independent pressure control for each chuck, with chucks near the cutting head operating at a lower force to minimize vibration transmission. Support rollers (steady rests) carry the tube weight, allowing lower clamping forces. For ultra‑thin tubes (D/t > 80), an internal mandrel is required.
Operators should calculate the D/t ratio and select clamping force from established tables, then fine‑tune based on test cuts. Ovality measurement before and after clamping validates the setup. By controlling deformation, the machine achieves consistent cut quality over the entire tube length.
Read More: Long‑term Tracking Data: Impact of Laser Power Decay on Cutting Speed
Frequently Asked Questions
Q: How do I know if the tube is slipping during cutting?
A: Monitor the rotary encoder feedback. If the actual position deviates from the commanded position by more than 0.5° repeatedly, slippage is occurring. Also, listen for squeaking or chirping noises from the chucks. Increase clamping force in 10% increments until slip stops.
Q: Can I use the same clamping force for aluminum tubes as for steel?
A: No. Aluminum has a lower friction coefficient (0.1–0.2) and lower modulus (70 GPa), so it deforms more easily. Use 40–60% of the force used for steel of the same dimensions, and use smooth or polyurethane jaws to avoid marking.
Q: What is the maximum allowable ovality for precision laser cutting?
A: For tube cutting, ovality should be ≤0.2% of diameter (e.g., 0.2 mm for a 100 mm tube) for high‑precision work, and ≤0.5% for general fabrication. Above 0.5%, the focus variation becomes significant.
Q: My machine has only two chucks. How is deformation control different?
A: Two‑chuck machines typically use higher clamping forces because there is no additional support. This severely limits their ability to cut thin‑wall tubes without deformation. Four‑chuck machines are superior for thin walls.
Q: How often should polyurethane chuck jaws be replaced?
A: Inspect every 500 cycles or 40 operating hours. Replace when the polyurethane shows cracks, indentation, or loss of elasticity. Worn jaws reduce friction and increase marking risk.
References
- Yihai Laser Cutting Machine Operation Manual. Section 3.1: Machine tool structure; Section 4.3: Exchange worktable (pneumatic principles applicable to chuck actuation). (Company internal document)
- XC3000S Series Laser Cutting System User Manual. Raytools AG. Section on pipe cutting module.
- HypCut Laser Cutting Control Software User Manual, Version 1.4. Section 4: Production – multi‑station machining.
- ISO 8493:1998. Metallic materials – Tube – Drift expanding test. (Reference for tube deformability)
- Laser Institute of America. (2021). Clamping Strategies for Tube Laser Cutting. LIA Technical Guide TG‑TUBE‑2021.
- Adams, S. M. (2005). Sheet Metal Bend Allowance. KETIV Virtual Academy. (General metalworking principles)
